2026 Best Sand Casting Parts Suppliers for Global Buyers?
Global buyers searching for the 2026 best Sand Casting Parts suppliers need more than a polished catalog. They need parts that meet drawing requirements, arrive on schedule, and perform reliably in service. Supplier selection can affect tooling costs, inspection workload, and production continuity.
This guide explains how to assess suppliers using practical criteria: casting materials, dimensional controls, machining options, quality documentation, lead times, and communication. A capable manufacturer should be able to discuss part geometry, likely casting challenges, and inspection methods in clear terms. Ask how the supplier manages patterns, sand preparation, pouring, finishing, and nonconformance reports. Details matter. A vague answer about “strict quality” is not the same as a measurable inspection plan.
Look beyond quoted price. Compare sample approval procedures, production capacity, packaging, and the support available when drawings change. Request relevant certificates and inspection records, then confirm that they apply to the process and facility handling your order. Where possible, review sample parts or arrange an independent inspection. No supplier is perfect, and published claims may not tell the whole story. That deserves a closer look. A low initial quote can become costly if rework, unclear specifications, or missed delivery dates follow. Use the supplier profiles and evaluation points ahead to build a shortlist, ask focused questions, and match each option to your part’s requirements. The best fit is not always the largest factory; it is the supplier whose capabilities, evidence, and communication suit your project.
Sand Casting Basics: Alloys, Molds, and ISO 8062 CT10–CT13 Tolerances
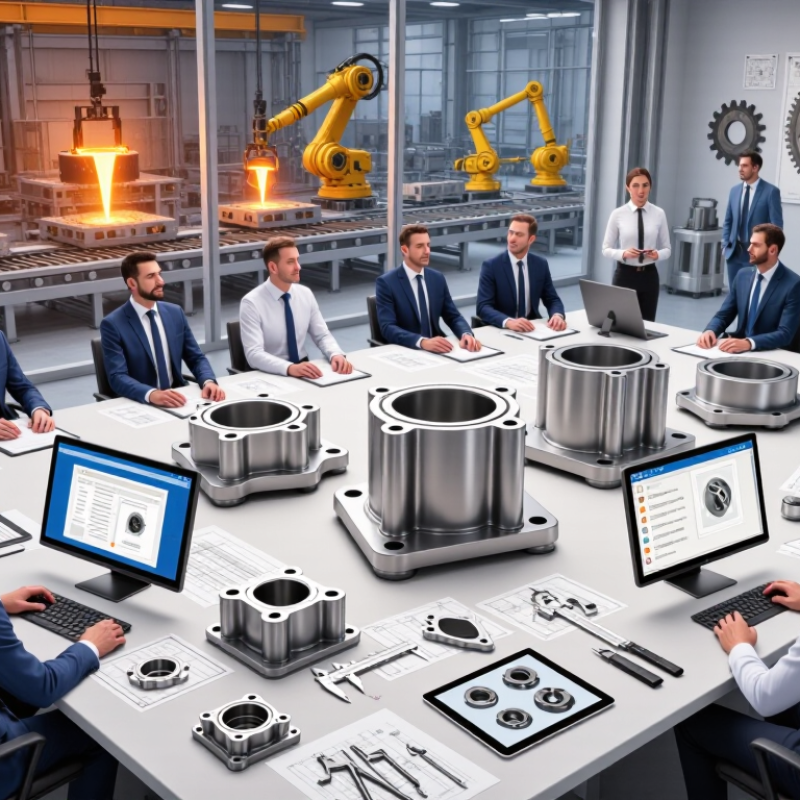
Sand casting begins with a pattern that forms a cavity in compacted sand. The mold may use green sand or chemically bonded sand, depending on part size, detail, and production volume. Aluminum alloys suit lighter components, while iron and steel alloys support heavier loads and higher service temperatures. Alloy choice affects more than strength. It also changes shrinkage, pouring behavior, and finishing needs.
ISO 8062 CT10–CT13 describes dimensional casting tolerance grades, not a promise that every feature will meet one value. The permitted variation depends on nominal size and the drawing requirements. CT10 is generally tighter than CT13, but tighter tolerances may require added machining, process control, or inspection. That matters. Buyers should identify critical dimensions, datum points, and machining allowances before requesting quotations. A vague note can create disagreement later.
For supplier reviews, ask how patterns, sand properties, and pouring conditions are monitored across production runs. Request sample inspection records for dimensions that affect assembly, such as a bearing seat or bolt-hole spacing. A first article can look excellent. Not every part will. Sand molds can shift, and metal shrinkage varies with geometry and process control. Even so, CT10–CT13 is a useful starting point when drawings and inspection plans define the real acceptance criteria.
2026 Best Sand Casting Parts Suppliers for Global Buyers? - Sand Casting Basics: Alloys, Molds, and ISO 8062 CT10–CT13 Tolerances
| Supplier Capability Profile | Common Sand-Cast Alloys | Molding and Production Strengths | Typical Tolerance Target | Useful Quality Checks | Best Fit for Buyers | What to Confirm Before Ordering |
|---|---|---|---|---|---|---|
| General-purpose green-sand foundry | Gray iron, ductile iron, and carbon steel, subject to the foundry’s melt capacity and specifications | Moist sand molds; practical for a broad range of part shapes and production quantities | CT12–CT13 is a reasonable initial discussion range for many conventional sand-cast features; confirm by dimension and drawing | Visual inspection, dimensional inspection, material test reports, and agreed mechanical tests | Industrial housings, brackets, covers, and other parts where cost and robust construction are priorities | Alloy grade, heat treatment, casting weight and envelope, machining allowance, and inspection plan |
| Resin-bonded sand foundry | Carbon steel, low-alloy steel, stainless steel, and iron grades, depending on equipment and melt practice | Bonded sand molds and cores can support complex internal passages and larger or heavier castings | CT11–CT13 may be proposed for as-cast dimensions; tighter requirements should be assessed feature by feature | Dimensional reports, visual inspection, and specified radiographic, magnetic-particle, or ultrasonic testing where appropriate | Pumps, valves, energy equipment, and large components with demanding internal geometry | Critical wall sections, core support, defect acceptance criteria, NDT coverage, and traceability requirements |
| Precision-focused no-bake or chemically bonded sand supplier | Commonly iron and steel casting alloys; availability depends on the supplier’s qualified process | Offers flexibility for prototypes, low-to-medium volumes, and parts requiring carefully controlled cores | CT10–CT12 may be a target for selected dimensions when the process and geometry support it; obtain a drawing-specific capability review | First-article dimensional inspection, process records, material certification, and agreed non-destructive testing | Custom components with complex geometry or more demanding dimensional control than a basic sand-cast part | Which dimensions are controlled as-cast, which are machined, and how the tolerance grade is applied to each feature |
| Aluminum sand-casting specialist | Aluminum casting alloys such as A356-type alloys, when specified and available | Sand molds and cores provide design flexibility for aluminum parts with cavities or irregular shapes | CT10–CT13 may be discussed according to part size, geometry, and process; machining is commonly used for precision interfaces | Alloy and heat-treatment certification when specified, dimensional inspection, and pressure or leak testing if required by the application | Lightweight housings, covers, manifolds, and low-to-medium-volume aluminum components | Exact alloy designation, temper or heat treatment, porosity limits, leak-test method, and machining datums |
| Integrated casting and machining supplier | Iron, steel, or aluminum grades matched to the part specification and available process route | Combines molding, casting, heat treatment where applicable, and machining in one coordinated supply chain | As-cast areas should have a separately agreed casting tolerance; machined features can be specified to their drawing tolerances | First-article inspection, dimensional reports, material records, and verification of machined datums and interfaces | Parts with critical bores, sealing faces, bearing seats, or other precision features | Machining scope, datum strategy, allowance, inspection responsibility, and control of revision changes |
| Prototype and low-volume sand-casting supplier | Selected iron, steel, or aluminum alloys depending on tooling, melt capacity, and qualification | May use patterns or tooling suited to prototype and short-run programs; confirm repeatability for future volume increases | CT12–CT13 is a practical starting point for many as-cast features; critical dimensions usually need explicit review or machining | Prototype dimensional report, material verification, visual examination, and agreed sample approval process | Design validation, replacement parts, pilot production, and smaller-volume custom orders | Pattern ownership, tooling changes, repeat-order consistency, lead time, and transition plan for production volumes |